
TOLERANCE & INSPECTION

Surface Profile Tolerance: Datums, Tolerance Zones, and CMM Inspection

Learn how to interpret surface profile tolerance, establish the datum reference frame, use nominal CAD data, and plan reliable CMM inspection.

TOLERANCE & INSPECTIONVIETTECH · TECHNICAL RESOURCES
01

What does a surface profile tolerance control?

A surface profile tolerance limits the deviation of an actual surface from its true profile. The true profile may be defined by basic dimensions on the drawing, a revision-controlled CAD model, or both. Unlike a size tolerance that controls one distance or diameter, profile can govern a continuous combination of curved, blended, inclined, and planar surfaces. Before quotation, the supplier must identify the exact controlled surface and the governing GPS or GD&T standard. A profile requirement is not a generic statement that every measured coordinate may vary by half of the stated value.

  • Surface profile tolerance — Dung sai biên dạng bề mặt — 面の輪郭度公差
  • True profile — Biên dạng danh nghĩa — 理論輪郭
  • Basic dimension — Kích thước cơ bản — 理論的に正確な寸法
  • Datum — Chuẩn — データム
02

How is the tolerance zone established?

Under common ASME Y14.5 application, the tolerance zone consists of two boundaries around the true profile. Unless unequal disposition or another specific requirement is shown, the zone is generally treated as equally disposed; the drawing must nevertheless be interpreted under its stated standard and edition. A 0.20 mm profile value should not automatically be converted into independent ±0.10 mm coordinate tolerances. Evaluation is based on the normal deviation of the actual surface from the nominal profile and on the required datum alignment.

Surface Profile Tolerance: Datums, Tolerance Zones, and CMM Inspection
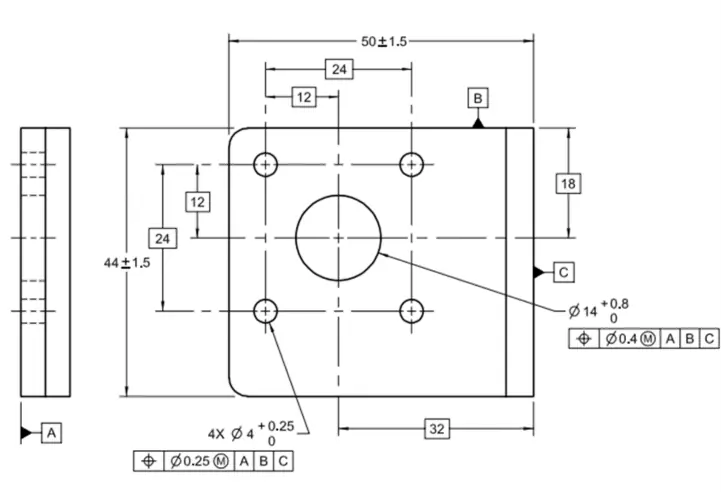
Technical diagram: Surface Profile Tolerance: Datums, Tolerance Zones, and CMM Inspection. This is not a production photograph; specifications and acceptance follow the drawing.

Profile without datum references

The control generally emphasizes surface form. The inspection alignment must still be agreed because an unconstrained best fit does not provide the same control as a defined datum reference frame.

Profile related to A–B–C

The profile requirement may control form, orientation, and location relative to the datum reference frame. Inspection must establish those datums in the specified order rather than best-fitting the measured surface to reduce error.

03

Role of the 2D drawing and CAD model

For a freeform or blended surface, the 2D drawing may identify the tolerance and controlled region while the nominal geometry resides in the STEP file or native model. Both files must carry the same revision. Any mismatch should be resolved before CAM or CMM programming. Excluded areas, boundary lines, datum targets, and surfaces outside the profile requirement should be explicit. A screenshot or tessellated STL file is normally inadequate for building a controlled nominal profile because it may not preserve exact geometry.

  • Keep the drawing and model at the same revision
  • Identify the controlled area with a leader or all-around/all-over indication where appropriate
  • Do not substitute a free best fit for the specified datum alignment
  • Confirm whether ISO GPS or ASME rules govern acceptance
04

Inspection methods for surface profile

A tactile CMM is commonly used to compare measured points or scan paths against nominal CAD geometry and generate deviation reports. Point density, probe direction, stylus diameter, scanning speed, filtering, and accessibility influence the result. Optical or laser scanning can capture denser data but requires control of reflectivity, surface finish, and measurement uncertainty. A contour measuring instrument or functional gage may be more efficient for a simple profile. Equipment must be selected according to tolerance magnitude, part size, surface geometry, and the intended acceptance decision.

Alignment before reporting

Alignment should reproduce the functional datum reference frame. Best fit is acceptable only when the drawing or approved inspection plan permits it.

Sampling strategy

Points or scan paths should cover curvature changes, blends, edges, and difficult-to-machine areas. Too few points may miss a local peak; indiscriminate oversampling increases cycle time without necessarily improving the decision.

05

Impact on the machining process

Surface profile is often applied to 3D faces, sealing surfaces, mating contours, or geometry that would be cumbersome to define with many separate dimensions. CAM planning must control interpolation tolerance, toolpath tolerance, cutter radius, tool deflection, stock distribution, and finishing sequence. A visually smooth surface may fail profile, while a surface within profile may still fail a separate Ra requirement. Profile and surface roughness are distinct controls and must be planned independently.

  • Balance stock during roughing before finish machining
  • Minimize tool overhang where possible
  • Use stable toolpaths through blends and curvature changes
  • Reinspect after unclamping when workholding force may distort the part
06

Common drawing and inspection errors

Frequent problems include missing datums for a located surface, undefined limits of application, mismatched CAD revisions, confusion between profile and roughness, and a tight tolerance without an agreed measurement method. CMM software may also report different values depending on alignment, filtering, point strategy, and how bilateral deviations are reduced to a single result. For repeat production, the parties should agree on datum alignment, scan paths or point density, excluded regions, reporting format, and applicable standard before the first lot.

  • Do not assume unilateral disposition unless the drawing states it
  • Do not assess a complex profile with only a caliper or a few micrometer checks
  • Account for stylus radius and probe access
  • Do not use profile as a substitute for every size and roughness requirement
07

Information to include in an RFQ

Complete input allows VietTech to review machining, programming, workholding, and inspection time before quotation. For a large surface or a small tolerance, CMM programming and measurement may be a significant part of total cost.

  • Controlled 2D drawing and STEP model at the same revision
  • Governing standard and edition, such as ASME Y14.5 or ISO GPS
  • Controlled surface and datum reference frame
  • Profile value, zone disposition, and datum modifiers when applicable
  • CMM report, color map, sampling density, or FAI requirements
  • Material, treatment, quantity, and required delivery date

RELATED PAGES

Hole-pattern position tolerance and MMC ↗Flatness vs. parallelism ↗Quality and inspection ↗

FAQ

Frequently asked questions

Is profile 0.20 equivalent to ±0.10?

It should not be converted into independent coordinate tolerances. Read the profile zone, zone disposition, datum references, and governing standard.

Can a CMM freely best-fit a profile without datums?

Not by default. The alignment method must reflect design intent and be agreed before acceptance.

Is a STEP file sufficient for profile inspection?

A drawing or controlled requirement is also needed to define tolerance, datums, scope, and revision.

Does passing profile guarantee the Ra requirement?

No. Profile controls macroscopic geometry; surface roughness controls texture at another scale.

Can VietTech inspect surface profile on a CMM?

VietTech reviews part size, access, tolerance, datum structure, and reporting requirements for each drawing.

TOLERANCE & INSPECTION

Have a profile-controlled surface to review?

Send the 2D drawing, 3D model, datum reference frame, profile requirement, material, quantity, and reporting needs for a machining and inspection review.REQUEST A QUOTE ↗