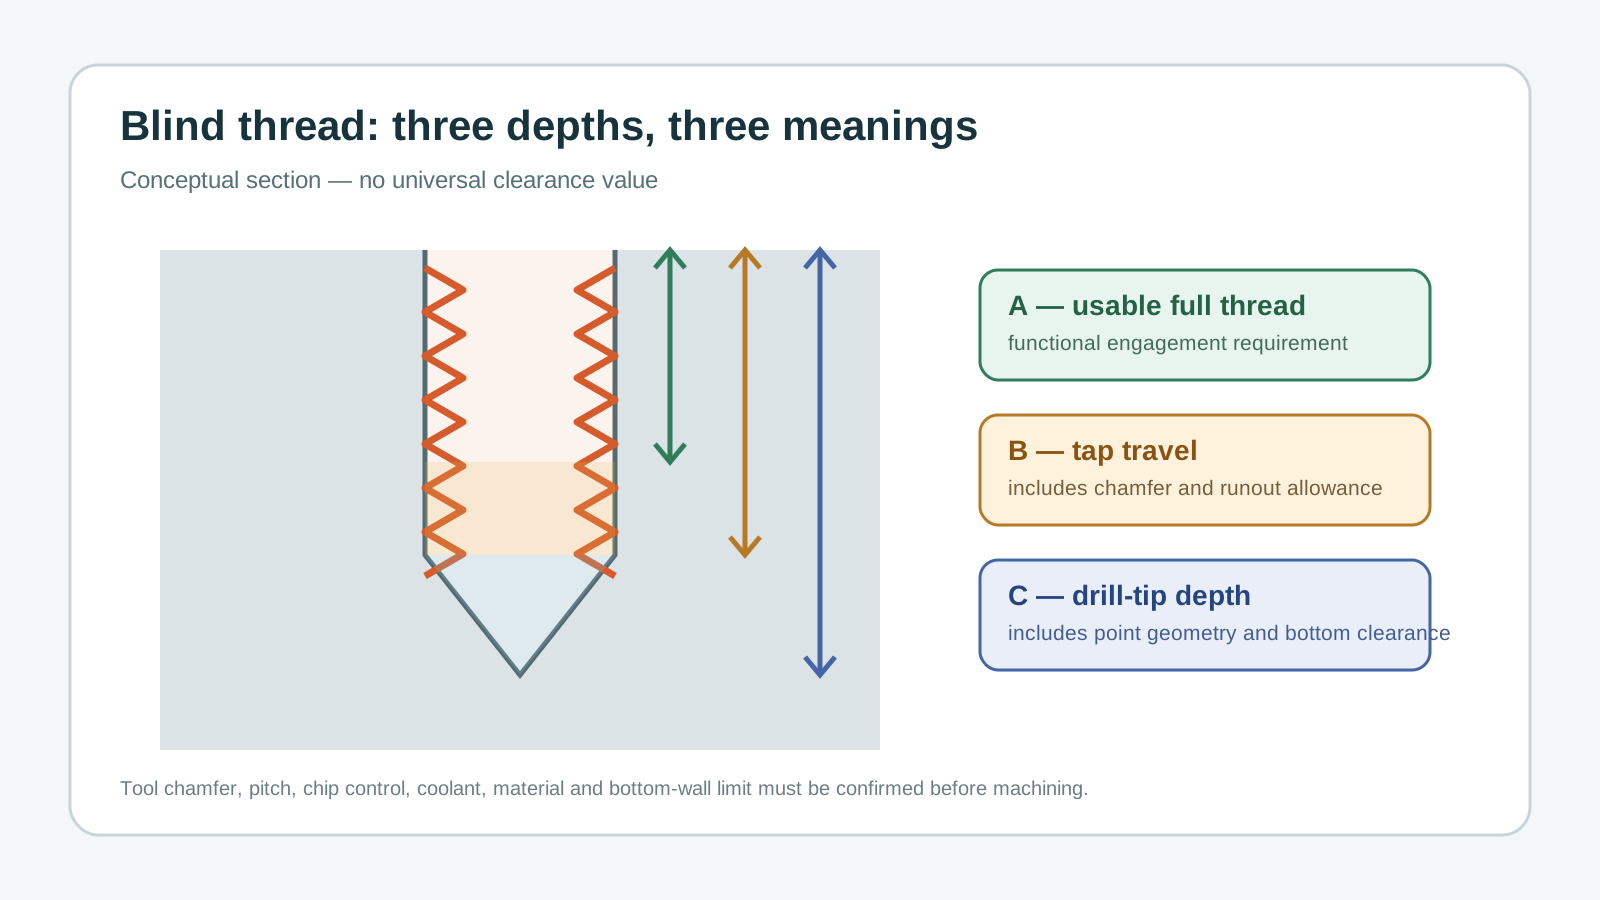
One blind threaded hole contains three different depths
A blind hole stops inside the part. At least three depths may matter: the usable full thread needed by the fastener, the tool travel needed to create that thread, and the drill-tip depth that includes the conical point. A callout such as “M6 depth 12” can mean different things to design and manufacturing. The result may be insufficient engagement, a bottom wall that is too thin, tool collision or compacted chips. Define the functional thread first, then identify any separate bottom limit that must be controlled.