
Overview
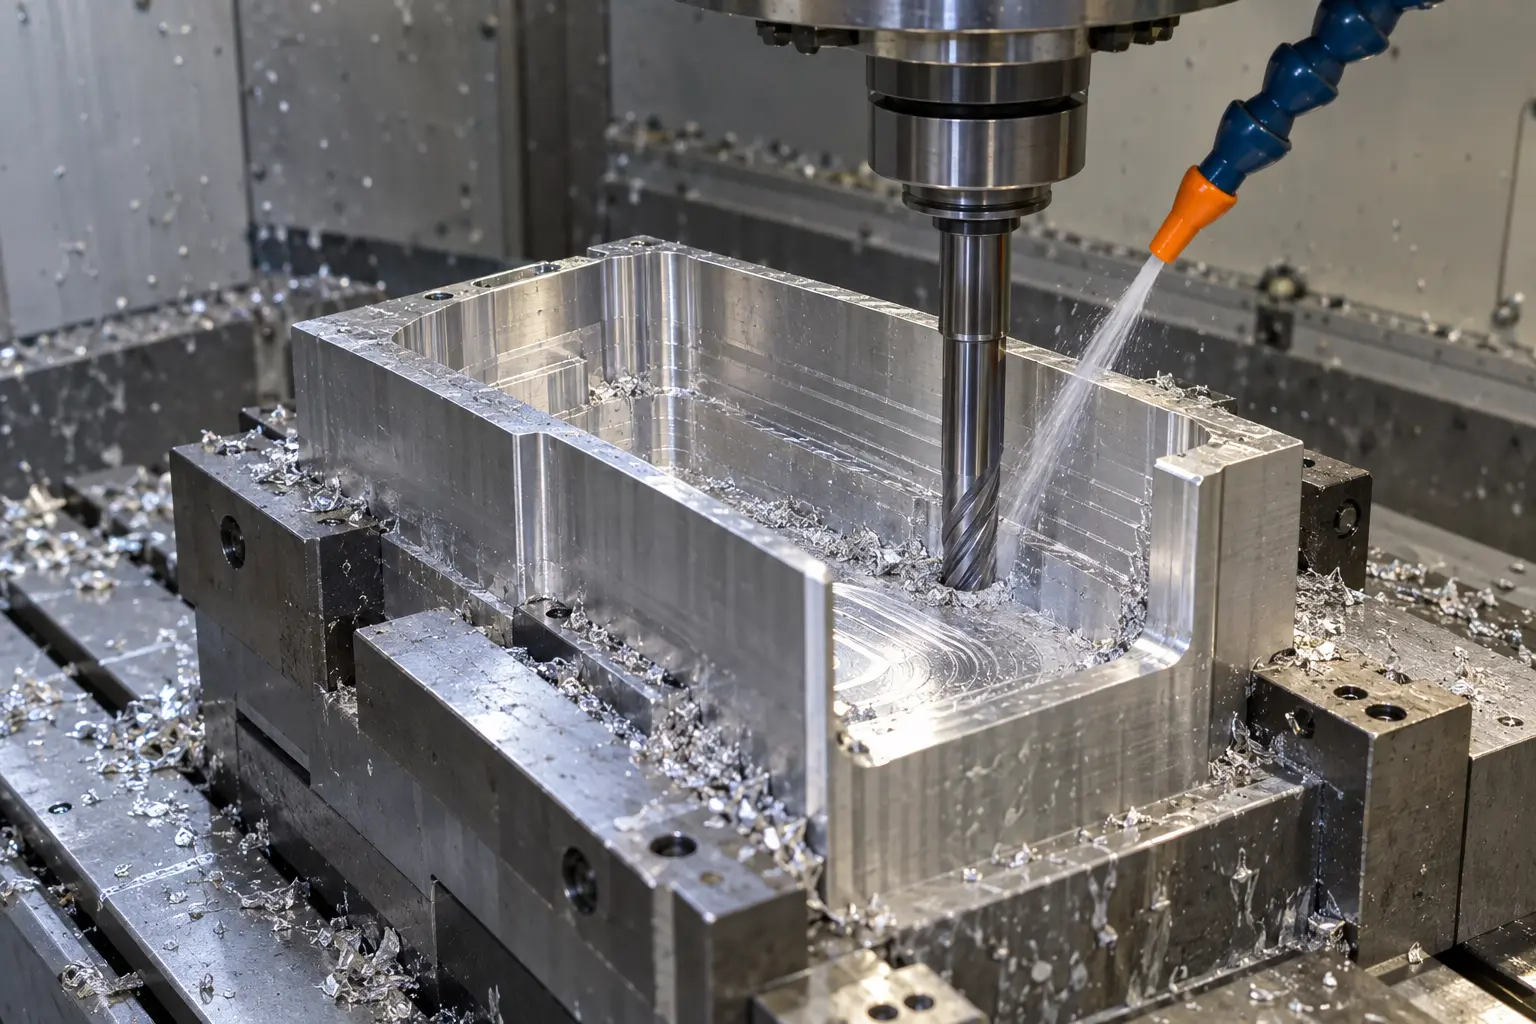
Deep pockets are common in machine bodies, housings, fixtures, mold components, and lightweight structural parts. The geometry may appear simple, but the process can be difficult to stabilize: the cutter requires extended reach, chips remain trapped, coolant access deteriorates, and tool deflection can produce tapered walls. A robust process does not begin by selecting the longest cutter and using it at full depth. Part design, tool overhang, roughing and finishing strategies, chip evacuation, allowance distribution, and inspection access must be evaluated together. These decisions influence cycle time, tool life, surface integrity, and dimensional capability.